
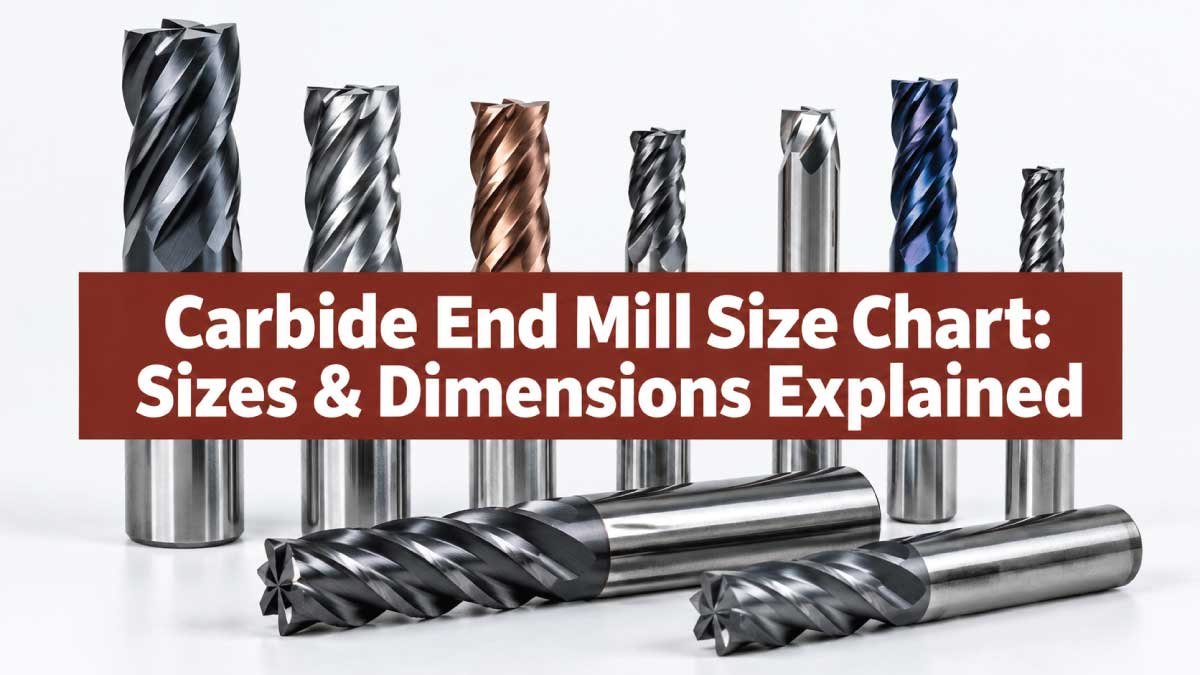
Choosing the correct cutter size is important for achieving accurate dimensions, clean surfaces, efficient material removal, and predictable tool life. A carbide end mill size chart helps machinists compare cutting diameters, flute lengths, shank sizes, and overall dimensions before selecting a tool for a particular milling operation.
Carbide end mills are available in many diameters and configurations, from very small micro tools used for precision work to larger cutters designed for heavy material removal. The correct size depends on the workpiece material, machining operation, machine capability, required depth, feature size, and desired finish.
This guide explains common carbide end mill sizes, important dimensions, flute configurations, end mill types, measurement methods, and practical selection considerations. Because manufacturers offer different geometries and dimensional combinations, the charts below should be treated as general size references rather than universal manufacturer specifications.
Understanding Carbide End Mill Dimensions
A carbide end mill is a rotary cutting tool used in milling machines, CNC machining centers, routers, and other machining equipment. Unlike a drill, an end mill can cut with its end, side, or both, allowing it to produce slots, pockets, contours, shoulders, profiles, and other features.
The most important dimensions are not limited to the cutter diameter. A tool that has the correct diameter but an unsuitable flute length or shank configuration may still be inappropriate for the job.
Key Dimensions to Know
When reading an end mill specification, pay attention to:
Cutting diameter: The diameter of the cutting portion.
Shank diameter: The diameter held by the tool holder or collet.
Flute length: The usable cutting length along the flutes.
Overall length: The total length of the tool.
Number of flutes: The number of cutting edges or helical flutes.
Helix angle: The angle of the cutting edge relative to the tool axis.
Corner geometry: Square, corner-radius, or ball-nose configuration.
Center-cutting capability: Whether the tool can perform suitable axial plunging operations.
Coating: A surface treatment selected according to the workpiece and machining conditions.
These dimensions work together. Increasing flute length, for example, may provide greater cutting depth but can also increase tool deflection compared with a shorter, more rigid tool of the same diameter.
Cutting Diameter vs. Shank Diameter
The cutting diameter determines the width of the tool’s cutting path under appropriate conditions, while the shank diameter is the portion secured in the holder.
They are not necessarily the same.
A small end mill may have a cutting diameter of only a few millimeters while using a larger shank, whereas some tools use a shank diameter that closely corresponds to the cutting diameter. Always check both measurements before purchasing a replacement tool.
Carbide End Mill Size Chart
The following chart provides representative commonly encountered cutter diameters. Exact flute lengths, overall lengths, and shank dimensions vary significantly among tool manufacturers and product families.
| Metric Cutting Diameter | Approx. Inch Equivalent | Typical General Use | Size Category |
|---|---|---|---|
| 1 mm | 0.039 in | Micro features | Micro |
| 2 mm | 0.079 in | Small slots and details | Small |
| 3 mm | 0.118 in | Precision profiling | Small |
| 4 mm | 0.157 in | General small features | Small |
| 5 mm | 0.197 in | Slots and pockets | Small |
| 6 mm | 0.236 in | General CNC work | Small/Medium |
| 8 mm | 0.315 in | Pockets and profiles | Medium |
| 10 mm | 0.394 in | General machining | Medium |
| 12 mm | 0.472 in | Roughing and profiling | Medium |
| 16 mm | 0.630 in | Larger pockets | Large |
| 20 mm | 0.787 in | Heavy material removal | Large |
| 25 mm | 0.984 in | Large-scale milling | Large |
These diameters are useful reference points, but they do not represent every available carbide end mill size. Intermediate, fractional-inch, specialty, and custom dimensions are also available.
Common Inch End Mill Sizes
In inch-based tooling systems, end mills are commonly identified by fractional or decimal diameters. Examples include:
| Inch Diameter | Approx. Metric Equivalent | General Application |
|---|---|---|
| 1/16 in | 1.59 mm | Small details |
| 1/8 in | 3.18 mm | Small slots and profiles |
| 3/16 in | 4.76 mm | Light general milling |
| 1/4 in | 6.35 mm | General-purpose work |
| 5/16 in | 7.94 mm | Slots and pockets |
| 3/8 in | 9.53 mm | General machining |
| 1/2 in | 12.70 mm | Larger pockets and roughing |
| 5/8 in | 15.88 mm | Heavy-duty applications |
| 3/4 in | 19.05 mm | Larger material removal |
| 1 in | 25.40 mm | Large milling operations |
Metric equivalents shown here are conversions, not necessarily the exact size of a commercially interchangeable tool.
Carbide End Mill Size by Flute Length
Flute length describes the portion of the tool where the cutting edges are formed. It is one of the most important dimensions when determining how deeply an end mill can machine a feature.
A longer flute does not automatically mean that the tool should be used at the maximum possible depth. Tool rigidity, workpiece material, machine stability, holder setup, and cutting parameters all affect practical performance.
Short Flute End Mills
Short flute tools provide a relatively compact cutting geometry and are often useful where the required cutting depth is limited.
Their shorter cutting length can help maintain rigidity and reduce unnecessary tool engagement. They are useful for shallow pockets, profiling, slotting, and finishing operations where deep reach is unnecessary.
Long Flute End Mills
Longer flute tools provide greater axial cutting capacity. They can be useful when machining deeper pockets or features that require extended cutting length.
However, excessive tool reach can increase deflection and vibration. The cutter should therefore extend only as far as necessary from the holder whenever possible.
Extra-Long Reach Tools
Extra-long-reach carbide end mills are designed for difficult-to-access features and deep cavities. Some are manufactured with reduced necks or specialized geometries to provide clearance.
These tools require particularly careful setup because the increased distance between the holder and cutting zone can make the tool more sensitive to vibration and deflection.
Carbide End Mill Size Chart by Flute Configuration
The number of flutes affects chip space, feed capability, surface finish, and the way the tool interacts with different materials.
| Flute Count | Typical Characteristic | Common Use |
|---|---|---|
| 1 flute | Large chip space | Plastics, non-ferrous materials, routing |
| 2 flute | High chip clearance | Aluminum, slotting, general work |
| 3 flute | Balance of chip space and strength | Aluminum and general milling |
| 4 flute | Greater edge engagement | Steel, finishing, general machining |
| 5+ flute | High tooth count | High-efficiency milling and finishing |
This table is a general guide rather than a rule. Modern end mills use specialized geometries, variable helix designs, chip breakers, coatings, and unequal flute spacing that can change how a tool performs.
Two-Flute End Mills
Two-flute cutters leave substantial space between cutting edges for chip evacuation. This makes them particularly common for slotting and machining materials where chip removal is important.
Four-Flute End Mills
Four-flute carbide cutters provide more cutting edges and can offer greater productivity or finishing capability in suitable applications. They are widely used for steels and other engineering materials.
For full-width slotting, however, chip evacuation requirements should be considered carefully rather than selecting a flute count based solely on the number of cutting edges.
Three- and Five-Flute Tools
Three-flute designs can provide a useful balance between chip space and tooth engagement, particularly in certain aluminum applications. Five-flute and higher-count cutters are frequently used for high-efficiency milling and finishing strategies.
The appropriate choice depends on the material and machining strategy.
Carbide End Mill Types and Their Dimensions
The phrase “carbide end mill” describes the tool material, not a single cutter geometry. Several end mill types use solid carbide construction.
Square End Mill
A square end mill has a flat cutting end and is commonly used for:
- Slotting
- Pocketing
- Profiling
- Facing
- Shoulder milling
- General contouring
The cutting diameter and flute length are usually the primary dimensions to compare.
Ball Nose End Mill
A ball nose end mill has a rounded cutting tip. It is frequently used for three-dimensional surfaces, molds, dies, curved profiles, and finishing operations.
The ball diameter and effective cutting geometry are important when selecting the tool for a particular surface.
Corner Radius End Mill
A corner-radius end mill combines a flat bottom with a rounded transition at the cutting corners. This geometry can reduce sharp-corner stress and is useful in profiling, pocketing, and finishing.
The corner radius must be considered in addition to the cutter diameter.
Roughing End Mill
Roughing cutters are designed to remove material efficiently. Their cutting geometry may include serrations or specialized chip-breaking features.
When comparing roughing end mills, consider diameter, flute length, number of flutes, and the manufacturer’s recommended application range.
Also Read:
How to Choose the Correct Carbide End Mill Size
Selecting an end mill should begin with the feature being machined rather than the tool diameter alone.
1. Match the Cutter to the Feature
Measure the slot, pocket, radius, wall, or contour that needs to be produced.
For example, a narrow slot may require a small-diameter end mill, while a large pocket may be more efficiently machined using a larger cutter followed by a finishing tool.
2. Consider the Required Cutting Depth
The flute length needs to accommodate the intended cutting depth while maintaining appropriate clearance.
Avoid selecting an unnecessarily long tool simply because it appears more versatile. A shorter tool can provide a more rigid setup when the application permits it.
3. Check the Machine and Holder
The tool must be compatible with:
- Spindle capacity
- Tool holder
- Collet or chuck
- Maximum spindle speed
- Available power
- Machine rigidity
- Work envelope
A correctly sized cutter can still perform poorly if the machine or tool-holding arrangement cannot support the operation.
4. Select the Flute Count for the Material
Material characteristics influence flute selection.
Aluminum and other materials requiring efficient chip evacuation may benefit from geometries with larger chip spaces. Harder materials may use higher flute-count tools and specialized carbide grades or coatings.
Always follow the tooling manufacturer’s application recommendations when available.
5. Consider Tool Reach
Use the shortest practical tool extension.
Excessive stick-out increases the leverage acting on the cutter and can contribute to deflection, chatter, poor surface finish, and premature tool failure.
Also Read:
How to Measure an End Mill
Accurate measurement is useful when identifying an existing cutter or checking whether a replacement tool matches the required dimensions.
Measure the Cutting Diameter
Use a suitable precision measuring instrument to measure across the cutting diameter. Measure at an appropriate point on the cutting portion rather than assuming the shank diameter represents the cutter size.
For worn tools, remember that measured dimensions may no longer represent the original manufacturer’s specification.
Measure the Shank Diameter
Measure the cylindrical shank where the tool is held.
This dimension must match the holder or collet system. A small difference between nominal and actual dimensions can matter in precision tooling applications.
Measure Flute Length
Measure from the end of the cutting portion to the point where the flute geometry ends.
Depending on the tool design, the transition may include a neck, relief, or other geometry, so it is better to compare the measurement with the manufacturer’s drawing when identifying a specific product.
Measure Overall Length
Overall length is measured from the cutting end to the opposite end of the shank.
This dimension is important for tool clearance, machine setup, tool changer compatibility, and reach.
Carbide End Mill Dimensions to Compare
When comparing two tools with the same cutting diameter, several other dimensions may determine which one is appropriate.
| Dimension | Why It Matters | What to Check |
|---|---|---|
| Cutting diameter | Controls cutter size and feature access | Required feature width |
| Flute length | Determines available cutting length | Required depth |
| Shank diameter | Determines holder compatibility | Collet/chuck size |
| Overall length | Affects reach and clearance | Machine setup |
| Flute count | Influences chip space and tooth engagement | Material and operation |
| Corner radius | Controls edge geometry | Drawing requirements |
| Helix angle | Affects cutting action and chip flow | Material and tool design |
| Coating | Influences tool suitability | Workpiece and application |
Looking at all of these dimensions gives a more complete picture than comparing diameter alone.
Also Read:
Carbide End Mill Size Selection for Different Materials
The same end mill diameter may behave differently in different materials. Tool geometry and cutting conditions should therefore be selected according to the workpiece.
Aluminum
Aluminum often benefits from tools designed for efficient chip evacuation. Two- and three-flute geometries are common choices, although the correct tool depends on the alloy, machine, operation, and manufacturer’s recommendations.
Sharp cutting edges and appropriate flute geometry can be important for controlling chip evacuation and surface quality.
Steel
Steel machining commonly uses solid carbide end mills with geometries designed for the specific steel grade and operation. Four-flute and higher-flute configurations are frequently encountered.
The tool diameter, flute length, coating, helix, and cutting parameters should all be considered together.
Stainless Steel
Stainless steel can present challenges related to heat generation, work hardening, and chip control. A purpose-designed carbide geometry may be preferable to a generic cutter.
Avoid assuming that a tool suitable for mild steel will automatically provide the same results in stainless steel.
Cast Iron
Cast iron machining may use carbide tooling designed for abrasive conditions. Tool geometry, edge preparation, coating, and coolant strategy can all influence tool life and surface finish.
Plastics
Plastics generally require attention to chip evacuation and heat management. Tool geometry should be selected according to the specific polymer because plastics can respond differently to cutting heat and friction.
Common Carbide End Mill Size Mistakes
Many tooling problems are caused by selecting a cutter based on only one specification.
Choosing Diameter Without Checking Flute Length
A cutter may have the correct diameter but insufficient cutting length for the intended feature. Conversely, an unnecessarily long flute can reduce rigidity.
Ignoring Shank Compatibility
Never assume that every cutter will fit every holder. Verify the shank diameter and holder system before installation.
Using Excessive Tool Stick-Out
Long projection increases the potential for deflection and vibration. Keep the tool as close to the holder as practical while maintaining the required clearance.
Assuming More Flutes Are Always Better
More cutting edges are not automatically better for every operation. Chip evacuation, material, feed rate, radial engagement, and machine capability all matter.
Treating a Size Chart as a Machining Parameter Chart
A size chart tells you about physical dimensions. It does not by itself determine the correct spindle speed, feed rate, depth of cut, or radial engagement.
Those parameters depend on the cutter design, workpiece, machine, holder, and manufacturer’s recommendations.
Carbide End Mill Size Chart: Quick Selection Guide
The following simplified guide can help narrow down the initial tool size.
| Machining Requirement | General Starting Consideration |
|---|---|
| Tiny precision feature | Small-diameter micro end mill |
| Narrow slot | Cutter close to required slot geometry |
| Shallow pocket | Short, rigid end mill |
| Deep pocket | Suitable flute length with controlled reach |
| Large material removal | Larger cutter or roughing end mill |
| 3D curved surface | Ball nose end mill |
| Sharp-bottom pocket | Square end mill |
| Reduced corner stress | Corner-radius end mill |
| Aluminum slotting | Chip-evacuating flute geometry |
| Steel profiling | Application-specific carbide geometry |
These are selection principles rather than universal machining prescriptions.
Carbide End Mill Size vs. Machining Accuracy
Tool size can influence machining accuracy because cutter diameter, rigidity, reach, and cutting forces interact.
A smaller end mill can access narrow features, but its smaller cross-section generally makes it more sensitive to deflection and accidental overload. Larger cutters are typically more rigid, but they cannot enter narrow features or produce small internal radii unless the geometry permits it.
For precision work, consider:
- Tool diameter
- Tool runout
- Holder condition
- Tool stick-out
- Machine rigidity
- Workholding
- Material properties
- Cutting forces
- Required tolerance
- Surface-finish requirements
For critical dimensions, the actual manufacturer’s tool drawing should be used rather than relying only on a general carbide end mill size chart.
Frequently Asked Questions
What are the most common carbide end mill sizes?
Common metric diameters include approximately 1, 2, 3, 4, 5, 6, 8, 10, 12, 16, 20, and 25 mm, while common inch sizes include 1/16, 1/8, 3/16, 1/4, 3/8, 1/2, 5/8, 3/4, and 1 inch. Availability varies by manufacturer and tool series.
What is the difference between end mill diameter and shank diameter?
The end mill diameter refers to the cutting portion, while the shank diameter refers to the portion secured in the tool holder. They can be different dimensions.
How do I choose an end mill diameter?
Start with the feature being machined. Choose a diameter that provides the required access and geometry, then consider flute length, rigidity, machine capability, material, and the intended machining strategy.
Is a larger carbide end mill always better?
No. A larger cutter can provide rigidity and material-removal capability, but it may not fit narrow features or small internal radii. The appropriate diameter depends on the workpiece and operation.
What is the best flute count for a carbide end mill?
There is no single best flute count for every job. Two- and three-flute tools can provide useful chip space in suitable applications, while four- and higher-flute tools are commonly used for other milling and finishing operations.
How much flute length do I need?
Use enough flute length to cover the required cutting depth and clearance. Avoid unnecessarily long cutting lengths because they can increase deflection and reduce rigidity.
Are metric and inch end mills interchangeable?
Not necessarily. Although their nominal dimensions can be converted mathematically, a metric cutter and a nearby inch cutter are not automatically interchangeable for precision machining. Match the actual required diameter and tool specifications.
What information should I check before buying a carbide end mill?
Check the cutting diameter, flute length, shank diameter, overall length, flute count, tool geometry, coating, corner style, material compatibility, and manufacturer’s recommended application range.
Final Takeaway
A carbide end mill size chart is most useful when it is treated as a starting point for comparing tool dimensions rather than as a substitute for a manufacturer’s specification sheet. Cutting diameter is important, but flute length, shank size, overall length, flute count, geometry, and application must also be considered.
For the best tool selection, first identify the feature you need to machine, then match the cutter diameter and cutting length to the geometry. After that, verify holder compatibility, tool reach, material suitability, and machine capability. For critical machining work, always confirm exact dimensions and recommended cutting conditions from the applicable tooling documentation.
Engineer Hassan is a Mechanical Engineer with 16+ years of hands-on experience in mechanical hardware, fasteners, and workshop tools. He focuses on size selection, thread identification, and measurement, helping users choose the correct components with accuracy and safety.